Filtration Consumable Reorder Points: How Much Spare Stock?
A filtration consumable reorder point should cover everything that happens between the moment stock falls to the trigger and the moment a replacement is accepted into the storeroom. That window includes the supplier’s production queue, packing, freight, customs release and your own receiving inspection, not just the transit time printed on a quotation. Two quantities set the trigger: the consumption expected across that window, and a reserve for the variation in both consumption and delivery. The reserve matters more than the average, because a press that stops for a missing cloth set costs more than the stock that would have prevented it.
What a reorder point has to cover
Three different quantities get called a reorder point in practice, and mixing them is why stock plans fail. The reorder point is the trigger level at which a purchase request is raised. Safety stock is the reserve held behind that trigger. Order quantity is how much one purchase covers. A fourth and fifth figure, the minimum and maximum levels, are gates that stop the trigger from being ignored or from overfilling the store.
The reason a trigger set at average lead-time demand runs out so often is arithmetic, not bad luck. Both consumption and lead time vary, so about half of all replenishment cycles will need more than the average amount of stock to cover them. The trigger has to be built from the demand across the window plus a reserve sized on the variation you have actually recorded.
| Quantity | What it defines | What changes it |
|---|---|---|
| Reorder point | Stock level at which a purchase request is raised | Consumption rate, lead time, chosen reserve |
| Safety stock | Reserve held against variation in demand and delivery | Recorded variability, cost of a stockout, storage limits |
| Order quantity | How much one purchase covers | Minimum order quantity, pack size, storage space, price breaks |
| Minimum level | Floor that should not be crossed | Reserve plus a receiving margin |
| Maximum level | Ceiling that pauses further buying | Storage capacity, shelf condition, working capital |
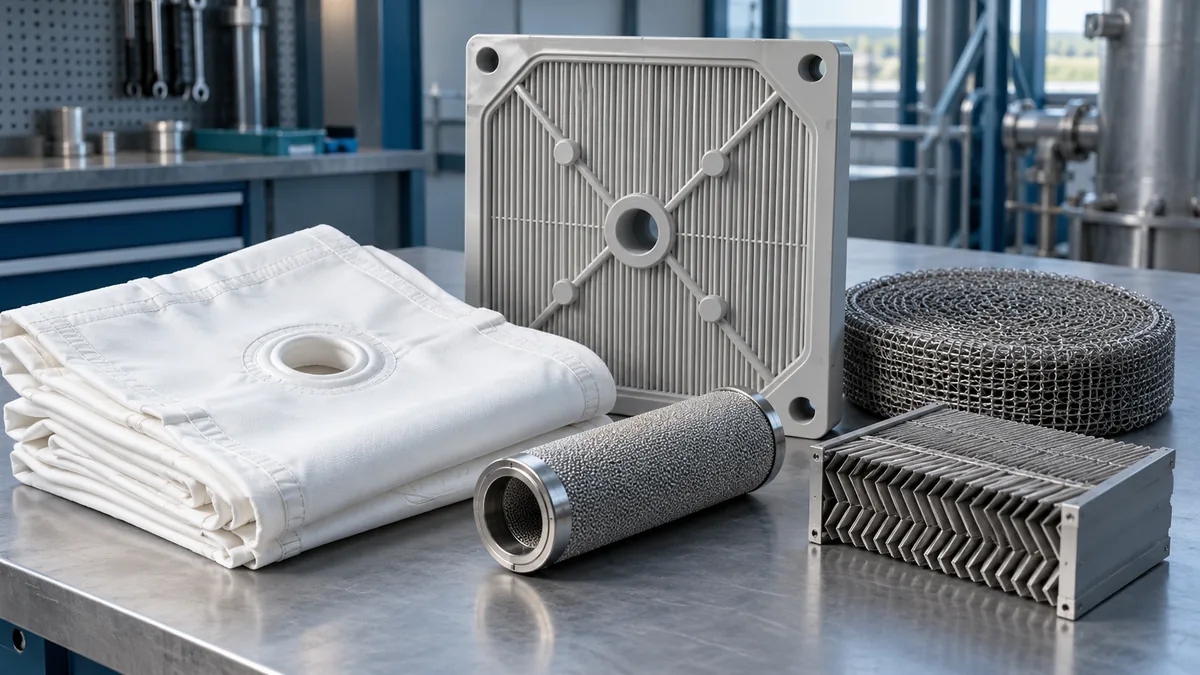
Which of the two inputs dominates depends on the item. A custom-cut cloth set or a moulded membrane plate is driven by lead time, because nothing about the ordering pattern changes how long production and delivery take. A cloth running in an abrasive slurry is driven by consumption, because issue rate can change within a few weeks of a feed change. Setting the trigger in the same unit the store uses when it issues stock, whether sets, pieces or square metres, prevents a conversion error at the worst moment.
Which lead-time components belong in the number
The clock that matters starts when the trigger is reached and stops when the item is released to the storeroom. Between those points sit several separate delays: internal approval and drawing confirmation, the supplier’s production queue, inspection and test reporting, packing, inland haulage, main freight, customs release, and your own receiving check. A supplier who quotes four weeks is often describing production completion, not a delivered and accepted item on your rack.
The practical way to build the number is to record it. For each purchase, log the date the request was raised, the order confirmation date, the production completion date, the shipment date, the arrival date, the customs release date and the date the item was accepted. Elapsed days across those milestones give you a distribution rather than a single figure, and the slowest realistic case in your own records is a better planning input than a quotation.
| Record | Method context | Responsible use | Do not infer |
|---|---|---|---|
| Quoted lead time on a supplier quotation | One specified standard item, at the time of quotation | A starting figure for planning | That a custom cut, non-standard gasket or revised drawing follows the same clock |
| Your own purchase history for the same item and supplier | Orders actually received and accepted | The strongest lead-time evidence you hold | That a different supplier, material grade or plant will repeat it |
| Supplier stock availability statement | Warehouse position checked on a stated date | Whether the item may ship without entering production | That the position will still hold when your purchase order lands |
| Freight forwarder transit estimate | Named route and mode, current at that time | Planning the transport leg only | That customs release, port congestion or inland haulage is included |
| Receiving inspection record | Your own acceptance check on arrival | Time from arrival to usable stock | That the first item will fit without a first-article check |
Each of these records describes the conditions under which it was taken. A quotation is a planning input, and a stock statement is a position on a date, not a commitment about your order.
How to convert consumption records into a demand rate
Consumption per calendar day is a weak number when the feed rate moves. The more reliable basis is consumption per unit of production: square metres of cloth per thousand tonnes of dry solids, cartridges per thousand operating hours, plates per press per year. Normalizing first means a seasonal or campaign-driven feed does not distort the rate you plan with.
Cloth life is best recorded in cycles, not weeks, because a press running more cycles per week consumes more cloth per week at identical cycle life. Issue records usually hold this information already, since stores issue cloth against a press and a date. Reading those records back over twelve months, and marking where a process change or a material change took effect, gives a rate that reflects how the plant runs now rather than how it ran two years ago.
Once the rate is expressed per production unit, convert it back into the ordering window. The working figure is consumption per day multiplied by the days from trigger to accepted stock, plus the reserve. If a plant issues four cloth sets in a ninety-day quarter and its recorded order-to-acceptance time is thirty-five days, the window figure is about 1.6 sets, and the reserve then has to absorb the weeks when the issue rate doubles. Those figures must come from your own issue records, because a rate borrowed from another plant says nothing about your slurry, cycle time or plate condition.
Setting the reserve for variability rather than average
Two variables, each with its own spread, combine into the reserve. A simple and defensible approach is to take the worst lead-time demand visible in your own records and hold the gap between that case and the average. A statistical approach using the standard deviation of demand across the lead time is also common where issue records are detailed enough to support it. Both need the same discipline: the reserve is sized on observed variation, not on a comfortable feeling about how much stock looks right.
The reserve carries a real cost, and not only working capital. Filter cloth stored in humid or dirty conditions can pick up contamination before it is fitted. Cartridge seals age on the shelf. Rubber membrane plates stored under load or near heat sources can lose the elasticity that the squeeze stage depends on. Deep stock of a slow-moving item therefore trades a stockout risk for a deterioration risk, and the trade should be made per item.
The exclusion condition is equally important. Where a stockout only delays a non-critical polishing filter, a thin reserve is rational and the money is better held as working capital. Where a stockout stops the press and the stack needs a complete plate set to run again, the reserve has to cover a full set, because a partial set has no operating value. Reviewing how often the reserve was actually consumed in the past year tells you whether the underlying rate or lead time is wrong, which is usually the real fault.
Which consumables deserve the deepest spare stock
Ranking consumables by unit price or by purchase frequency misplaces stock almost every time. The useful ranking combines the consequence of running out with the time needed to recover, and then checks whether any substitute exists on site. A low-cost item with a long production lead time and no substitute can be more critical than an expensive item available from a supplier’s warehouse.
| Consumable | What a stockout stops | Replenishment character | Stocking note |
|---|---|---|---|
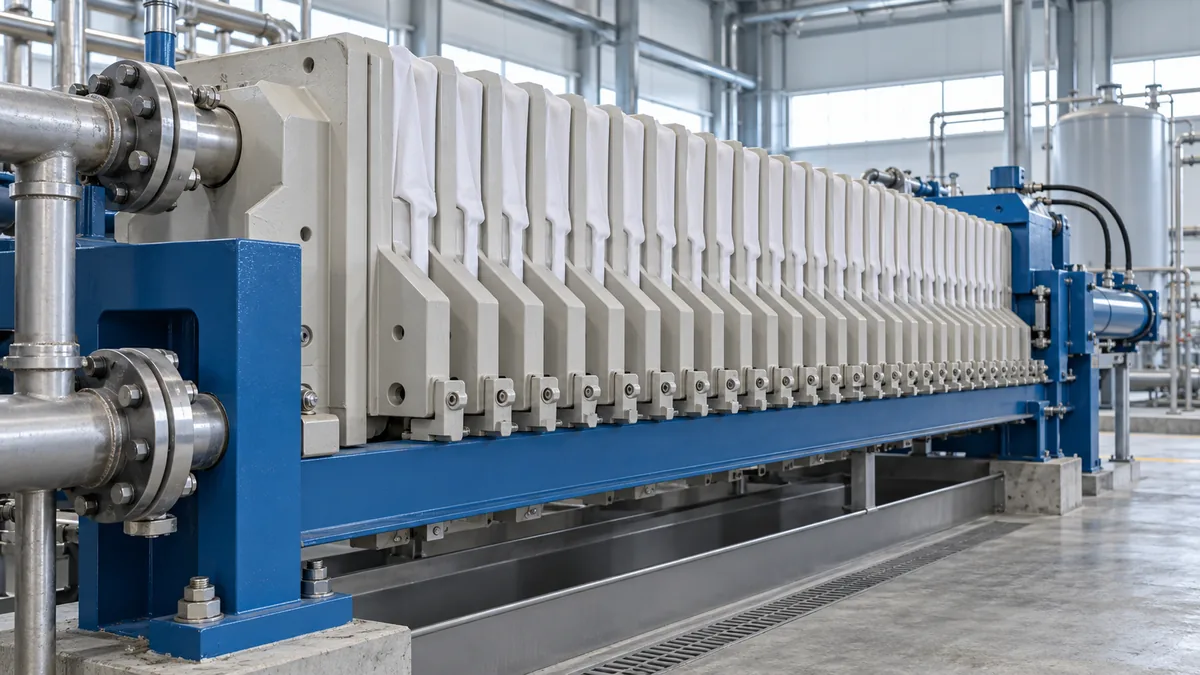
| Filter cloth set for one press | The whole press until a full set is fitted | Often cut to plate size and to order | Hold complete sets rather than partial sets |
| Filter plate in a specific size | Stack completeness, since plates are clamped as a set | Standard or custom depending on size, material and port layout | Decide the spare per size, not per total plate count |
| Rubber membrane plate | The squeeze stage and final cake dryness | Longer where vulcanization is to a non-standard size | Store flat, away from heat and ozone sources |
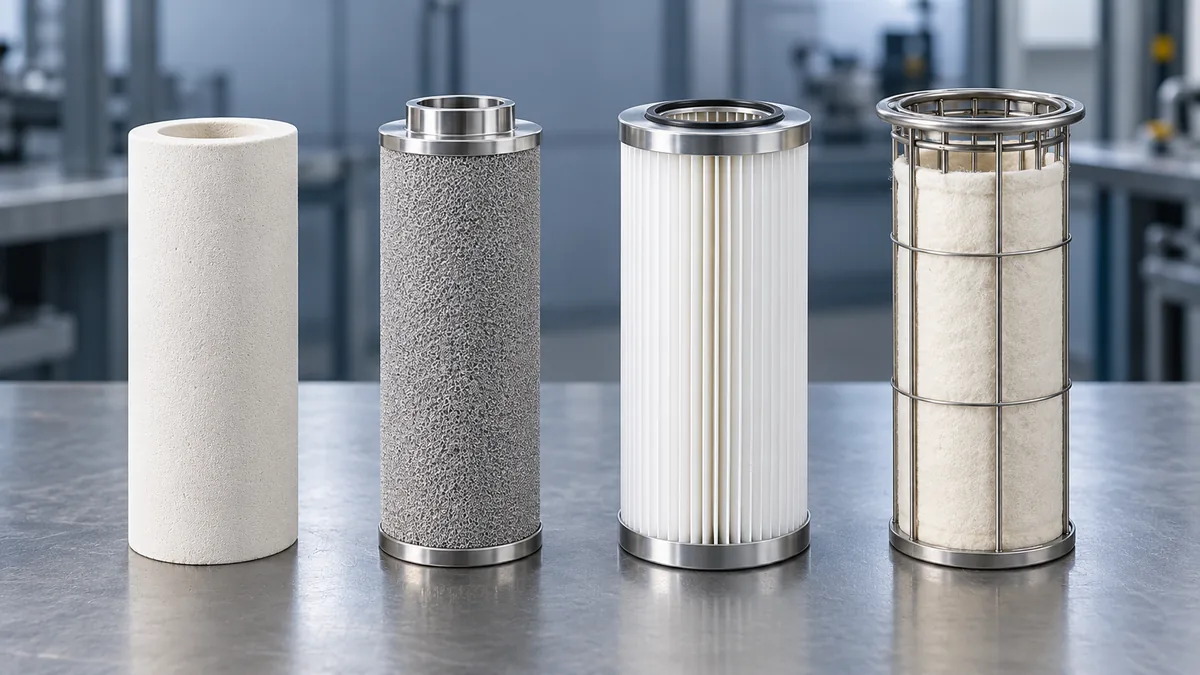
| Industrial cartridge set | A dust collector compartment or a process line | Media, end caps and seals are all specified together | Keep sealed against humidity and track seal age |
| Demister pad or vane pack | Vessel internals, and only fixable during a shutdown | Made to vessel dimensions with grids and fasteners | Align the spare with the shutdown calendar |
Material envelopes decide whether a substitute is a spare at all. A polyester cloth rated to 120°C and pH 4 to 9, a polypropylene cloth rated to 85°C and pH 1 to 13, and a nylon cloth rated to 100°C and pH 5 to 11 are not interchangeable across those limits. Stocking a substitute that sits outside the operating envelope creates an item that looks like insurance and fails when it is used.
Planning around shutdowns and peak season
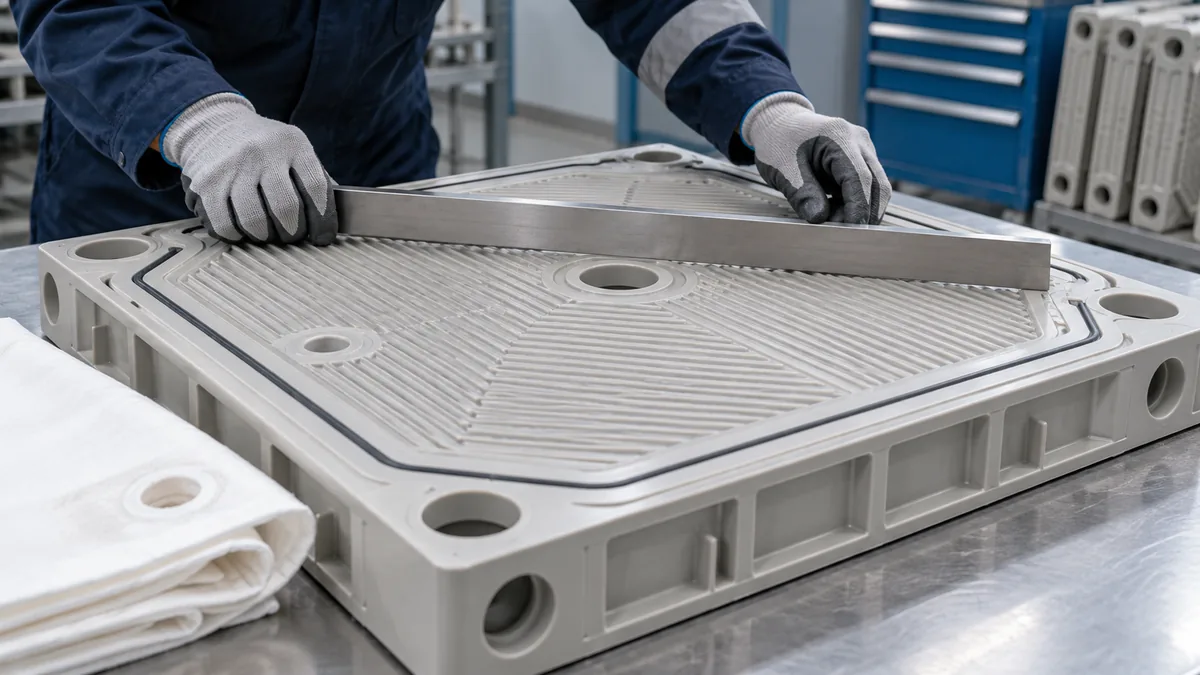
Consumption is lumpy. A shutdown consumes a full cloth set and often a plate inspection at the same time, and many plants schedule maintenance in the same few months, which lengthens supplier queues exactly when demand rises. A trigger based on average daily consumption is slow to react to an event that consumes several weeks of stock in one shift.
The event-based version works backwards from the shutdown date. Take the recorded lead time for that item, add your receiving margin, and the result is the date the purchase must be released. Adding a second offset for drawing approval or first-article acceptance keeps custom items from arriving after the work has started.
Freight mode is a separate trade. Air freight shortens the transport leg but the production queue in front of it does not move, so it recovers days rather than weeks and costs more per kilogram of cloth or plate. Consolidating cloth, plates and pads into one shipment reduces freight and customs handling, at the cost of coupling their arrival dates, which is unhelpful when one item is holding up the schedule and the others are not yet needed.
What to confirm with the supplier before you fix the number
Ask what the lead-time figure is based on: which specification, whether it covers production only or delivery, and whether a drawing approval step sits inside it. Confirm the minimum order quantity and pack size, because they decide the real order quantity when your calculated figure falls below the commercial minimum. Confirm what documentation arrives with the batch, because receiving cannot release stock into the store before it is checked.
| Current request | Replace with |
|---|---|
| Please quote your best lead time for filter cloth. | Quote production and delivery time separately for the specified plate size, material and model, state whether drawing approval is included, and give the minimum order quantity and pack size. |
| Please keep a spare in stock for us. | State which items you hold, in what quantity, checked on what date, and what triggers a restocking order. |
| RFQ field | What to state | Why it changes the number |
|---|---|---|
| Item identity | Material, model, dimensions and drawing revision | A close variant with a different face, port layout or gasket is not a substitute |
| Quantity basis | Sets, pieces or square metres, with the unit defined | Order quantity must match how the press actually consumes the item |
| Lead-time basis | Production only, ex-works, or delivered and accepted | Mixing bases shortens the figure you plan with |
| Transport and packing | Freight mode, consolidation, protection for plates and pads | Packing time and damage claims extend the arrival window |
| Acceptance documents | Test report, batch identification, dimensional record | Stock cannot be released without them |
Build the reorder list before the next shutdown
Send one list that a supplier can answer in a single pass: the item and specification with model or drawing revision, the unit you consume it in, your recorded order-to-acceptance time, the quantity you plan per order, the shutdown or campaign date it must support, and the documentation you need on arrival. With those fields, a replacement quotation can state production time, delivery time and minimum quantity separately instead of a single figure that hides where the weeks go.
Give the same list to the Shine Technology filtration team through shinefiltration.com, and ask for the basis of each lead time and the material envelope for every substitute offered, so the reorder point you set rests on numbers you can defend.
FAQ
Should a reorder point be a quantity or a date?
It is a quantity, because stock is issued in units and the trigger has to be visible in the store. The date version is a planning overlay: for shutdown-driven items, work backwards from the event using the recorded lead time and your receiving margin. Running both keeps a level trigger for routine cloth and cartridge issues and an event trigger for full sets and vessel internals.
How often should reorder points be recalculated?
Recalculate when an input changes rather than on a fixed calendar. Feed rate, slurry chemistry, cycle time, plate condition, supplier, freight mode and minimum order quantity all move the number. A short annual review catches slow drift, and a review after any process change catches the step change that a routine check would miss.
Do plates, cloth and cartridges use the same reserve logic?
They use the same method with different inputs. Cloth is consumed steadily and its reserve is sized on issue variability. A plate is consumed rarely but stops the stack, so its spare is a completeness decision rather than a rate calculation. Cartridges sit between the two, since a compartment can often run at reduced load while a replacement is in transit.
What if the minimum order quantity exceeds my calculated order quantity?
Buy the minimum and treat the surplus as reserve, then check whether the surplus degrades in storage. Cloth, seals and rubber plates all have storage sensitivities, so a large minimum can turn a stock decision into a shelf-life decision. Where the surplus is unusable before the next reorder, the honest options are a different pack size or a supplier who will supply below the minimum.
Can a supplier hold stock against my forecast?
Some can, and the arrangement needs the same discipline as your own store. Ask what quantity is held, for which specification, checked on what date, and what notice you must give to call it off. A holding arrangement that is not documented becomes a lead-time claim you cannot verify, which is no better than the quotation it replaced.